Food packing paper is a crucial component in the food packaging industry, designed to protect and preserve food while ensuring compliance with safety standards. Selecting the right food packing paper involves understanding various factors such as material type specifications and application suitability. This article will guide purchasing managers, distributors, and other industry professionals through the essential aspects of food packing paper including cost considerations, installation guidance, eco-friendly options, and supplier evaluation.
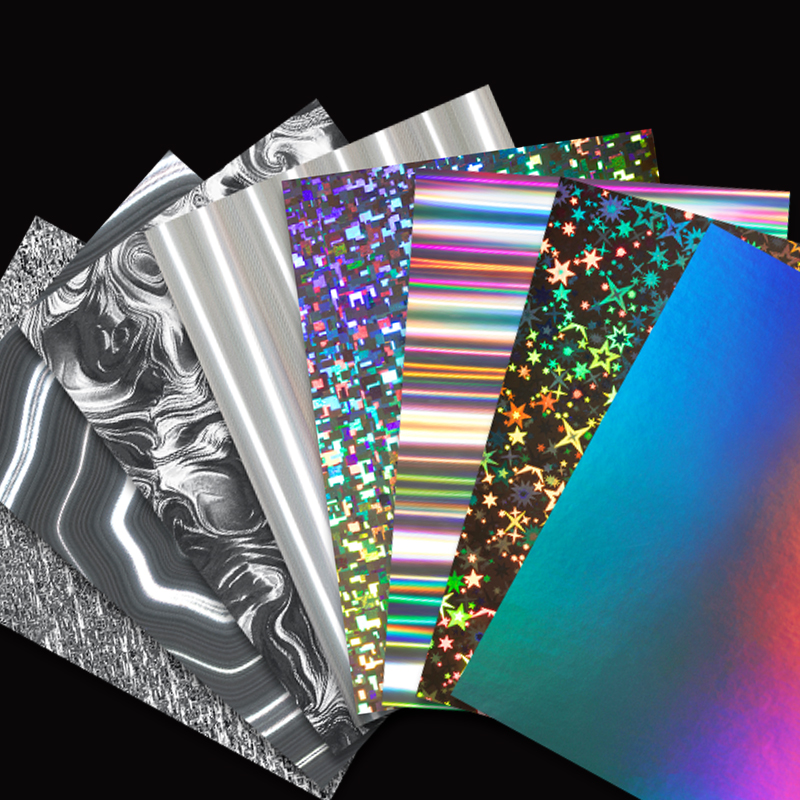
When selecting food packing paper, it’s essential to consider several key factors that directly affect performance and application. First, assess the type of food to be packaged. Different food items have various moisture and fat content levels, which necessitate specific barrier properties. For instance, greasy foods may require papers with superior grease resistance. Next, evaluate the thickness and weight of the paper. Thicker papers may offer better structural integrity and protection during transportation, while lighter papers might be more cost-effective for specific applications. Additionally, consider the paper's compatibility with printing and labeling needs, as some recycled packing paper can easily accommodate branding requirements. Finally, the environmental impact of the food packing paper should also be a consideration. With increasing consumer demand for sustainable packaging solutions, opting for recyclable and biodegradable materials, such as Shunho Creative's eco-friendly TransMet paper, can not only meet customer expectations but also enhance brand reputation.
Cost is a significant factor in any purchasing decision, but it should be balanced with quality and specifications. When assessing the cost of food packing paper, consider the following:
Material: The raw materials used in production can greatly influence price. For example, papers with advanced barrier properties, like Shunho Creative's laminated paper or TransMet paper, may come at a higher initial cost but offer better protection and shelf life, potentially reducing waste and spoilage.
Minimum Order Quantities (MOQ): Suppliers often have MOQs that can influence overall cost. Ordering in bulk can reduce unit costs, but it’s crucial to ensure that the volume aligns with your operational needs.
Quality Control Processes: Understanding the manufacturer’s quality control measures is vital. Papers that undergo rigorous testing and adhere to industry standards will likely perform better in real-world applications. Requesting certifications and quality assurance documentation from suppliers can help verify their claims.
Proper installation and usage of food packing paper can significantly impact its effectiveness. Here are some practical tips for ensuring efficient use:
Storage: Keep food packing paper in a dry, cool environment to prevent moisture absorption and degradation. Humidity can weaken the paper structure and compromise its barrier properties.
Handling: When handling recyclable packing paper, be mindful of preventing contamination. Use clean tools and gloves to maintain hygiene standards, particularly in food processing environments.
Sealing and Wrapping: Ensure that food items are sealed correctly using appropriate sealing methods. This can involve heat sealing or adhesive tapes, depending on the paper type. Proper seals prevent air and moisture ingress, extending the shelf life of the packaged food.
By adhering to these installation and usage guidelines, businesses can optimize the performance of their food packing paper, ensuring food safety and quality.
Adopting eco-friendly food packing paper comes with multiple advantages that resonate with both businesses and consumers. Here are some key benefits:
Sustainability: Eco-friendly papers, such as Shunho Creative's TransMet paper, are designed to be fully recyclable and degradable. This reduces the environmental footprint and aligns with global sustainability goals, appealing to eco-conscious consumers.
Compliance with Regulations: Many regions are tightening regulations on packaging materials, emphasizing the need for sustainable solutions. Using eco-friendly food packing paper helps businesses comply with these regulations, avoiding potential penalties.
Consumer Preference: As consumers become increasingly aware of environmental issues, they tend to favor brands that demonstrate a commitment to sustainability. Offering eco-friendly packaging can enhance brand loyalty and attract new customers.
Performance: Eco-friendly gift packing box papers can provide excellent barrier properties, ensuring food safety without compromising on quality. Advanced technologies, such as vacuum transfer metal, enhance the performance of these materials.
With FSC, REACH, FDA 21 CFR 176.170, (EU) No 10/2011, TUV OK COMPOST HOME, Silver holographic paper, ISO 9001/14001/45001, CNAS, PATENTS and other environmental protection certificates
More than 20 years of foreign trade experience.Laser paper is produced at a capacity that could reach around Holographic sticker paper tons per year.
Support for English, Spanish and Japanese Holographic stickers paper.
The majority of customers come Holographic stickers paper the leading 500 businesses in the world.
Choosing the right supplier for food packing paper is critical to ensuring quality and reliability. Here are some factors to consider when evaluating potential suppliers:
Reputation and Experience: Research the supplier's track record in the industry. A well-established supplier, like Shunho Creative, known for its innovative and eco-friendly packaging solutions, is likely to provide better quality and service.
Quality Certifications: Look for suppliers with relevant certifications, such as ISO standards or compliance with food safety regulations. This ensures that the materials meet necessary safety and quality benchmarks.
Customer Support: Assess the level of support provided by the supplier. Reliable suppliers should offer technical assistance, be responsive to inquiries, and provide clear communication throughout the purchasing process.
Flexibility and Customization: Consider the supplier's ability to accommodate custom orders or specific requirements. Flexibility in production capabilities can be crucial for businesses with unique packaging needs.
By conducting thorough evaluations and considering these factors, purchasing managers and industry professionals can make informed decisions, ensuring that they receive high-quality food packing paper that meets their operational requirements.
 EN
 AR
 HR
 CS
 DA
 NL
 FI
 FR
 DE
 EL
 HI
 IT
 JA
 KO
 NO
 PT
 RU
 ES
 TL
 ID
 VI
 HU
 TH
 TR
 MS
 GA
 CY
 MK
 HY
 PL